
From T0 Trial to Production Approval: How Molded Parts Are Validated
Meta title: From T0 Tooling Trial to Production Approval | ZED
Meta description: Understand how custom molded rubber and plastic parts progress through initial tooling trials, dimensional review, process adjustment and production approval.
Excerpt: The first tooling trial is not the end of development. It is the first opportunity to confirm how the real material, mold and production process work together.
What does the first tooling trial prove?
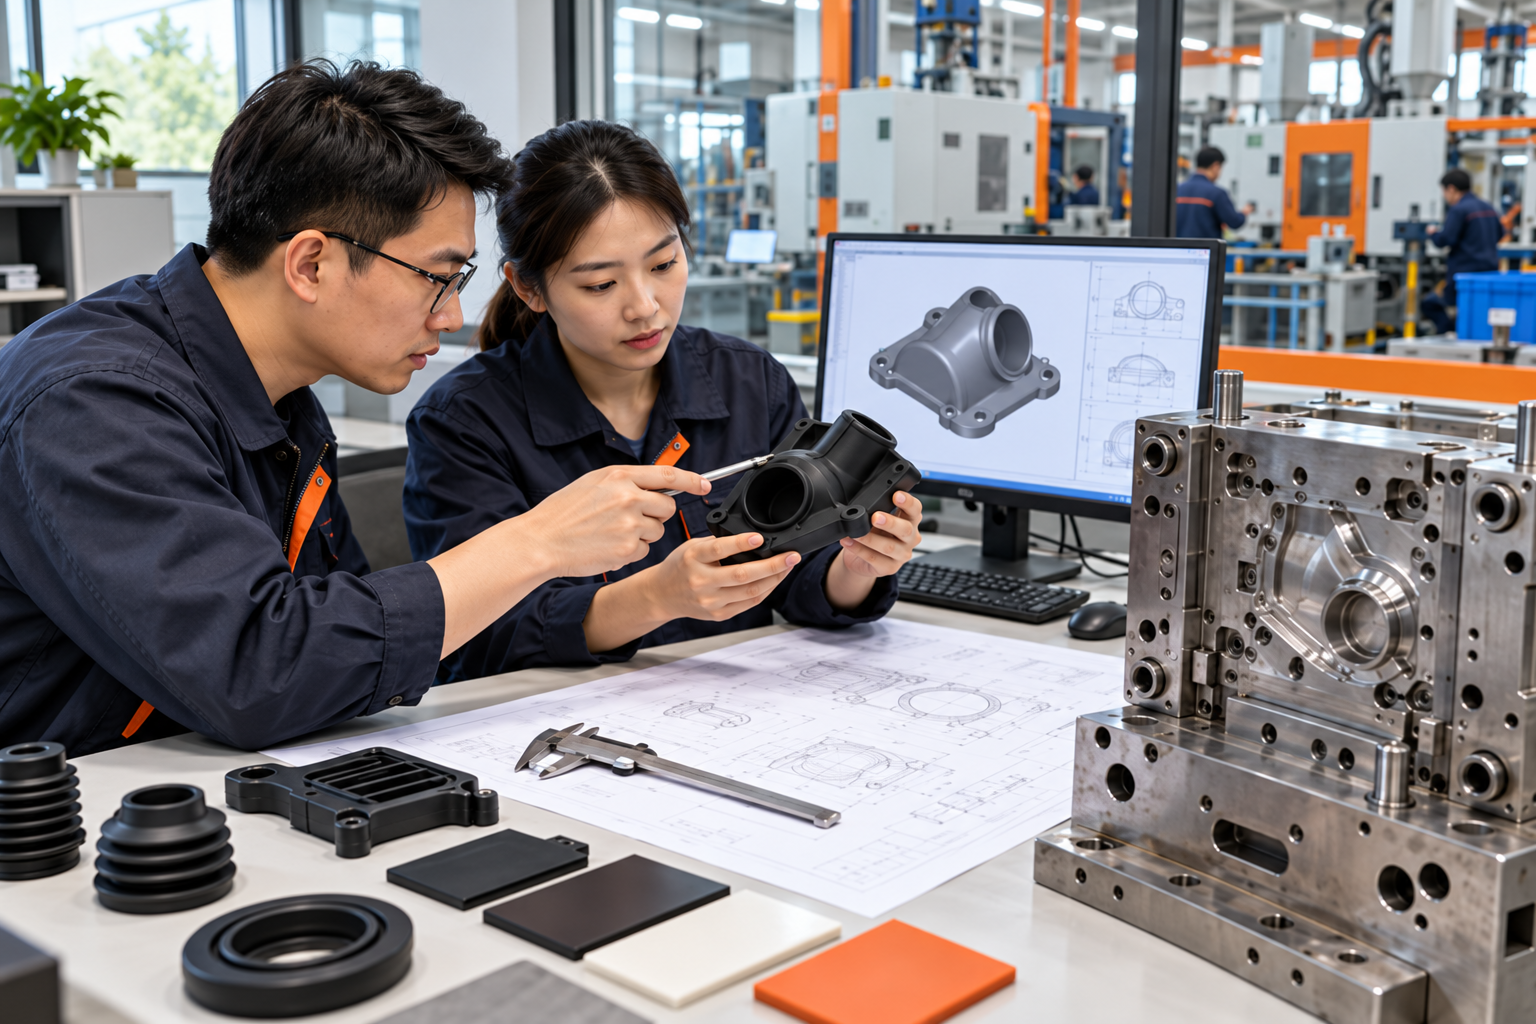
After a production mold is completed, the first trial is often called T0. The exact naming system can vary, but the purpose is similar: run the actual tool, observe its behavior and produce the first molded samples for evaluation.
T0 does not automatically represent the final production standard. It provides evidence for the next engineering decisions.
The trial should answer three basic questions:
Can the tool fill and release the part?
Does the molded part meet the functional and dimensional requirements?
Can the process become stable enough for repeatable production?
Stage 1: Prepare the correct trial conditions
A meaningful trial requires controlled inputs. The team should confirm the intended material grade or compound, material lot, color, mold configuration and planned process route.
For thermoplastics such as nylon, TPE or TPU, drying and moisture control may be critical. For compounded rubber, material identity, storage condition, preparation and cure behavior should be controlled.
Using an unapproved substitute material may help check basic tool movement, but the resulting dimensions and appearance may not represent the final product.
Stage 2: Observe filling and molding behavior
During the trial, engineers evaluate more than whether the cavity becomes full.
They review:
Filling balance and flow path
Short shots or trapped air
Flash and overflow
Weld or flow lines
Gate condition
Cure or cooling behavior
Ejection or demolding
Surface reproduction
Cycle stability
Photographs, process settings and observations should be recorded. This creates a useful baseline for later adjustments.
Stage 3: Allow the part to stabilize before measurement
Some molded parts change after removal from the tool. Cooling, internal stress, moisture absorption or post-curing can affect dimensions and properties.
The inspection plan should define when the part is measured and under what conditions. Measuring one sample immediately and another after conditioning can produce different results.
Flexible parts also need a consistent measurement method. If the measuring force deforms the part, results may vary between inspectors.
Stage 4: Compare the sample with the approved requirements
Sample review should cover four areas.
Dimensions
Measure critical dimensions first. General dimensions can then be reviewed according to the drawing and agreed tolerance standard.
Appearance
Check color, texture, gloss, flash, gate marks, sink, deformation and other visible conditions. Cosmetic acceptance should be based on an agreed reference rather than personal preference alone.
Function
Evaluate assembly, movement, sealing, grip, flexibility, fit and other product-specific functions.
Material performance
Confirm relevant characteristics such as hardness, recovery, tear behavior, adhesion or other project-specific tests.
Stage 5: Classify the required corrections
Trial findings usually fall into different categories:
Process adjustment: temperature, pressure, loading, injection speed, cure time or cooling
Tool adjustment: venting, gate, fit, cavity surface, insert or ejection
Part-design adjustment: wall thickness, draft, rib, radius, tolerance or interface geometry
Material adjustment: grade, hardness, formulation, drying or color system
Correctly identifying the source of the problem prevents unnecessary tool changes. A dimensional issue may be caused by process instability rather than cavity size. A bonding problem may come from material incompatibility rather than the mold.
Stage 6: Conduct the next trial with controlled changes
The next trial should not change many unrelated variables at the same time. Controlled changes make it easier to identify which action improved or worsened the result.
Each trial should record:
Tool revision status
Material and batch
Process conditions
Sample quantity
Dimensional results
Functional and appearance findings
Remaining actions
This trial history supports future production troubleshooting and repeat orders.
Stage 7: Establish the approved sample and production window
Production approval should identify more than one “good-looking” sample. The team should confirm an achievable process window and define the approved standard.
The approval package may include:
Approved sample
Final drawing and revision
Approved material and color
Critical dimensions
Functional test method
Cosmetic criteria
Key process conditions
Packaging and labeling requirements
The exact documentation level should match project risk and customer requirements.
Common trial mistakes
Projects often lose time when teams:
Approve appearance without checking function
Measure parts before they stabilize
Change material and process at the same time
Modify tooling before confirming the root cause
Fail to record trial settings
Approve one sample without evaluating repeatability
Leave packaging and assembly checks until mass production
A trial is part of process development
The purpose of tooling trials is to transform a newly built mold into a controlled production process. Samples, measurements and engineering decisions must remain connected.
ZED coordinates tooling, material, molding and inspection so that trial findings can be converted into practical production standards.


